Case Study: 2 T/H Cable Recycling Line Shipped to Europe
Case Study: 2 T/H Cable Recycling Line Shipped to Europe
Published in News & Insights · Case Study
By Henan Jiacui Intelligent Equipment Co., Ltd.
Overview
Item | Detail |
|---|---|
Project | 2 T/H (2,000 kg/h) Complete Cable Recycling Line |
Destination | Northern Europe (EU member state) |
Client | Mid-to-large WEEE & scrap-metal recycling operator |
Core throughput | 2,000 kg/h mixed waste cable |
Copper purity (output) | ≥99.5% standard / 99.8%+ on fine wire |
Configuration | Dual-line dry granulation + upstream shredding + dust collection |
Status | Shipped & commissioned |
When a European recycler came to us needing to process 2 tonnes of mixed waste cable per hour, the conversation was never going to be about a single machine. No standalone granulator in our range reaches 2,000 kg/h — and that is by design. The right answer for high-volume European operations is a complete, dual-line, dry-process recycling plant.
This is the story of how we engineered, built, and shipped that plant.
The Client's Challenge
The customer operates a licensed WEEE and metal-recycling facility in Northern Europe, processing end-of-life electrical equipment, automotive harness, communication cable, and household wire. Their existing single-machine line had plateaued, and three pressures were converging:
Volume. Inbound cable had grown to ~16–20 tonnes per 8-hour shift — well beyond what a single granulator could handle reliably.
Purity. Their copper buyer required ≥99.5% purity, with fine hair-wire and enameled wire pushing toward 99.8%+. Anything less meant a direct price discount at the smelter gate.
Compliance. As an EU-permitted facility, the plant is bound by the WEEE Directive (Directive 2012/19/EU, amended by Directive (EU) 2024/884), which requires all treatment plants to be officially licensed and sets minimum recovery targets — collection targets rising toward 65% of WEEE generated . It also faces local limits on noise and particulate emissions, pushing buyers toward enclosed dust collection and soundproofing .
Burning and wet separation were non-starters. The brief was clear: double the throughput with zero wastewater and no drop in purity.
The Solution: A Dual-Line Plant Around the RC-CWG1000
To reach 2 T/H with a safety margin, we specified two parallel processing lines, each centered on an RC-CWG1000 Copper Wire Granulator (900–1,000 kg/h). Running together, the twin lines deliver 1,800–2,000 kg/h — and the redundancy means a service stop on one line does not halt production.
System Layout
[ Infeed Conveyor ]

        ↓

[ Double-Shaft Shredder — primary pre-cut ]

        ↓

[ Magnetic Separator — remove steel / armored fractions ]

        ↓

   ┌────┴────┐

[ RC-CWG1000 Line A ]   [ RC-CWG1000 Line B ]   ← twin parallel granulators

    crusher → gravity → vibrating screen          each 900–1,000 kg/h

   └────┬────┘   └────┬────┘

        ↓

[ Pulse-Jet Baghouse Dust Collection — shared / zoned ]

        ↓

[ Copper granules │ Plastic regrind — separate outlets ]
Key Components
Upstream: Double-Shaft Shredder (Model 400, Dual-Drive)
JZQ250 reducers × 2, 4 kW × 2 (8 kW total), 20 blades (Φ160 mm)
Pre-cuts long cables, bulky harnesses, and armored lead into manageable lengths
Why it matters: feeding full-length cable directly into a granulator wraps and jams the rotor. Pre-cutting stabilizes downstream throughput and extends SKD-11 blade life to 600–1,200 h per regrind
Primary Separation: Twin RC-CWG1000 Granulators
Parameter | Each Line | Combined |
|---|---|---|
Output Capacity | 900–1,000 kg/h | 1,800–2,000 kg/h |
Main Crusher | 55 kW | 110 kW |
Blades | 18 × SKD-11 | 36 × SKD-11 |
Air system | VF fan 4kW×2 + dust fan 4kW×2 | Full dual circuit |
Gravity Separator | 6 kW | 12 kW |
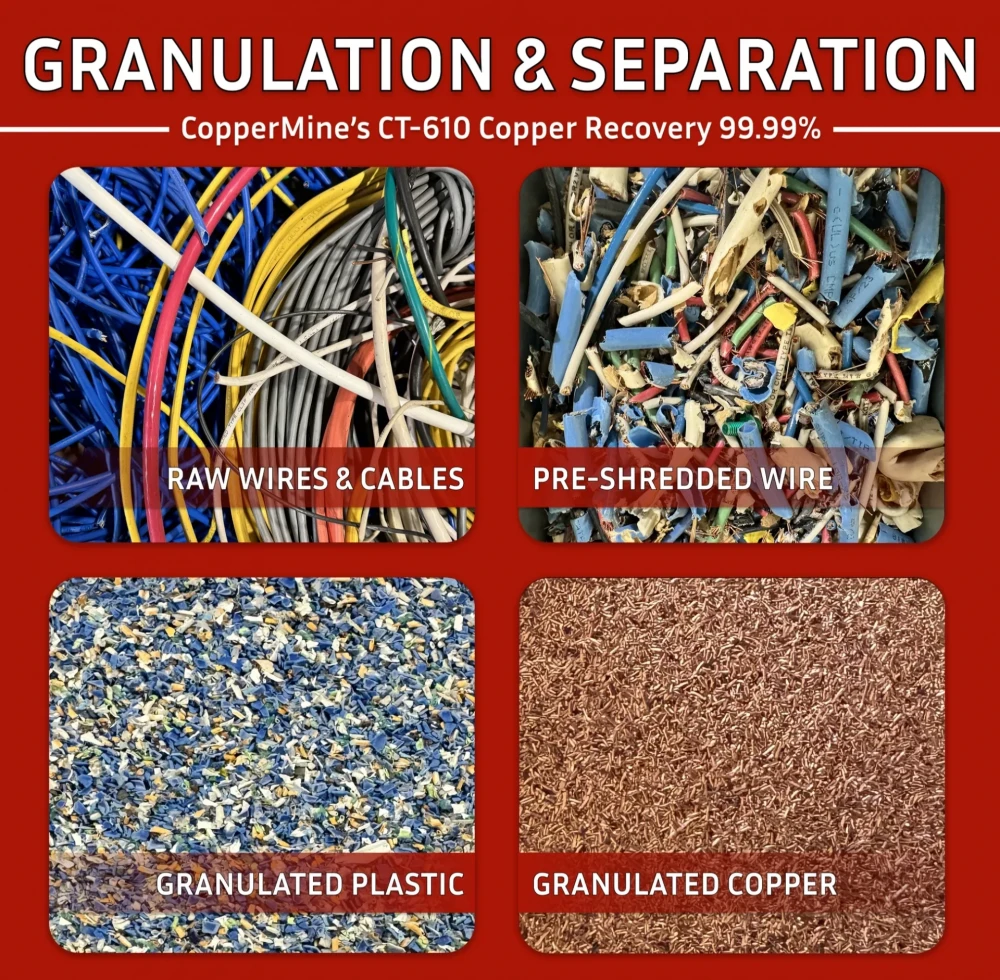
Each line executes the full dry process: crushing → airflow gravity separation → vibrating-screen refinement → optional electrostatics, holding ≥99.5% copper purity (99.8%+ on fine wire with the electrostatic stage).
Dust Collection: Zoned Pulse-Jet Baghouse
Captures fines at source across both lines; closed-loop, keeping the workspace within local particulate and ≤85 dB(A) operator-zone limits — the latter a core requirement under the EU Machinery Directive (2006/42/EC) and Noise Directive 2000/14/EC .
Control: Centralized PLC + VFD
One operator per shift oversees both lines via a Siemens/Schneider-class PLC with HMI; VFDs auto-adjust rotor speed and airflow to wire diameter (0.2–30 mm), trimming power draw versus fixed-speed designs.
Engineering for European Compliance
A line destined for the EU is more than a collection of machines — it is a documented, certified system. We engineered this project around the regulatory floor from day one.
CE Marking & Applicable Directives
The complete line was built to carry CE marking, with the technical file addressing:
Machinery Directive 2006/42/EC — guarding for cutting zones, anti-jam features, emergency stops, stability
EMC Directive 2014/30/EU — electrical systems
Low Voltage Directive 2014/35/E